46
National patents
Mannington commercial carpet tiles are engineered for high‑traffic interior environments where durability, acoustic performance, and ease of maintenance are critical. The product line supplied from
Order this product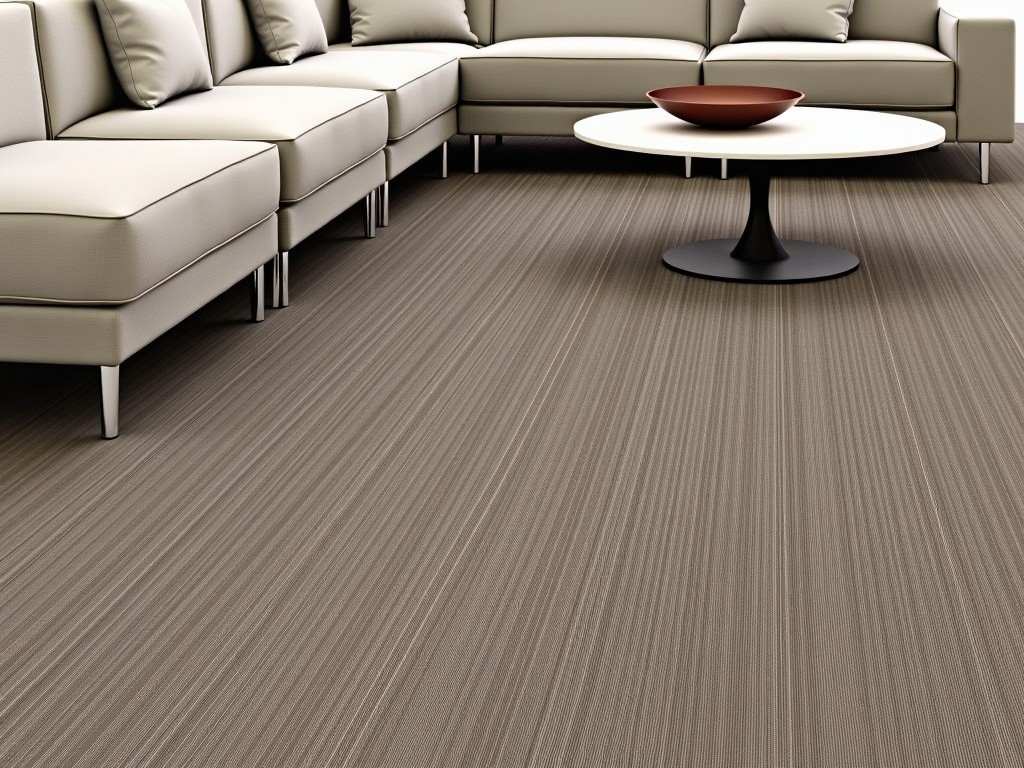
Mannington commercial carpet tiles are engineered for high‑traffic interior environments where durability, acoustic performance, and ease of maintenance are critical. The product line supplied from China combines tufted pile construction with a reinforced polyvinyl chloride (PVC) backing to meet the dimensional stability requirements of raised‑access flooring systems.
Tile dimensions are typically 500 mm × 500 mm with a tolerance of ±0.5 mm, allowing seamless integration with standard grid systems. The pile height ranges from 3 mm to 6 mm depending on the selected style, influencing both wear resistance and sound absorption coefficients.
The face yarn is solution‑dyed nylon or polypropylene, providing inherent stain resistance and UV stability. Yarn linear density is specified in denier (typically 1100–1500 dtex) to achieve a target pile weight of 400–600 g/m².
The backing consists of a PVC layer laminated with a fiberglass scrim, delivering a tensile strength of ≥15 MPa and a dimensional change of less than 0.2 % after 24 h exposure to 70 % RH at 23 °C. This backing also contributes to the tile’s fire‑rating classification (often Bfl‑s1 per EN 13501‑1).
| Property | Typical Value | Test Method |
|---|---|---|
| Pile Weight | 450 g/m² | ISO 1766 |
| Tuft Bind Strength | ≥15 N | ISO 4919 |
| Static Load Indentation | ≤0.15 mm after 24 h at 500 Pa | ISO 3416 |
| Impact Sound Reduction (ΔLw) | 20–25 dB | ISO 10140‑3 |
| Slip Resistance (R value) | R10 (wet) | EN 13893 |
Values above represent typical ranges for standard product grades; actual figures may vary with pile height, yarn type, and backing thickness. Custom specifications are available upon request.
In each setting, the tile’s dimensional stability reduces joint movement, while the backing’s resistance to moisture prevents delamination when installed over raised access floors with underfloor services.
Tiles are designed for glue‑down or loose‑lay installation using pressure‑sensitive adhesives compatible with PVC backings. Substrate flatness should not exceed 2 mm deviation over a 2 m straightedge to avoid telegraphing.
Expansion gaps of 5–10 mm are recommended at perimeter walls and fixed obstacles to accommodate thermal movement. Seam sealing tapes may be applied in areas exposed to frequent wet cleaning.
Post‑installation, a rolling load of 50 kg / 0.01 m² for 10 minutes verifies adhesion adequacy before traffic is permitted.
Manufacturing follows ISO 9001‑based process controls, with in‑line monitoring of pile height, gauge, and backing thickness. Each batch undergoes a random sample test for tuft bind and dimensional change after conditioning.
Finished tiles are inspected for color consistency using a spectrophotometer (ΔE*ab < 1.5) and for surface defects under 10× magnification. Packaging includes edge protectors and humidity‑barrier film to prevent deformation during transit.
Documentation such as material safety data sheets (MSDS) and test reports are provided with each shipment upon request.
Pile composition, dye lot, and backing thickness can be adjusted to meet specific performance targets such as higher sound absorption (ΔLw ≥ 30 dB) or increased load resistance for heavy equipment areas.
Custom logos or patterns are achievable through solution‑dyed yarn insertion or digital printing on the pile surface, subject to minimum order quantities typically starting at 500 m².
Lead times for customized orders range from 4 to 6 weeks, depending on design complexity and raw‑material availability.
Tracking information and customs documentation are provided electronically; cargo insurance can be arranged on request.
For detailed specifications, sample requests, or project‑specific consultation, please reach out to our technical support team.
Request Technical Data SheetNational patents
Vinyl flooring line
K+ SQ.M capacity
Founded